logo
Supal (Changzhou) Precision Tools Co.,Ltd
私たちに関しては
あなたのプロフェッショナルで信頼できるパートナーです
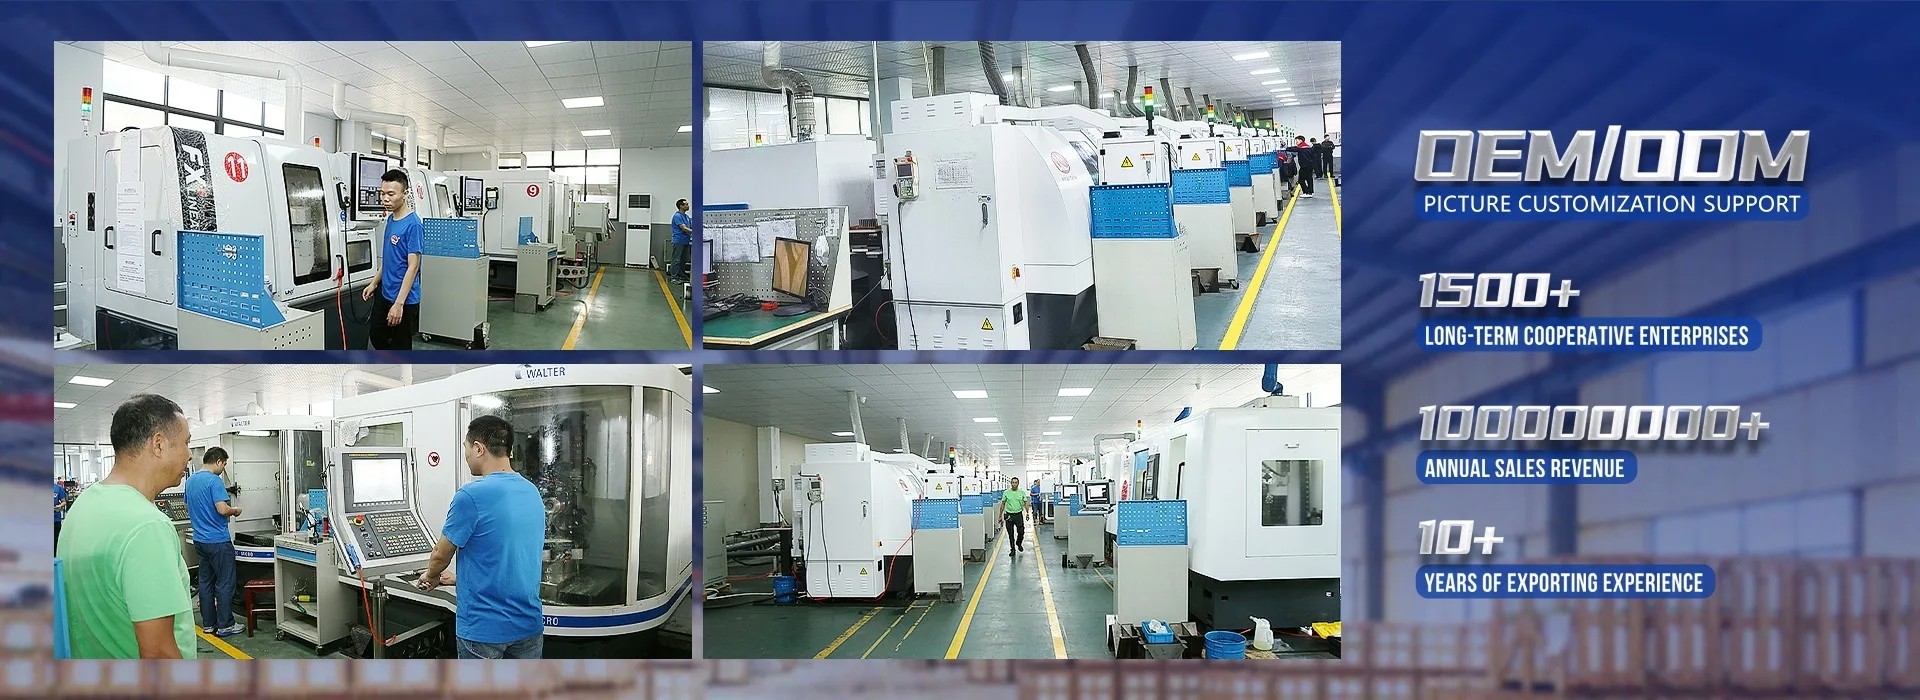
スーパール (チャン州) 精密ツール株式会社長年,固体カービッド工具の設計,生産,販売に従事しており,総投資額は1000万円以上で,経験豊富な従業員で構成されています.専門的なツールメーカーとして,それは長州Xiaxiashuツール協会の取締役メンバーの1つになりました. 会社はドイツのウォルターとシュッテを導入しました.オーストラリアのANCAと5軸NC切削機さらに,同社はZOLLERのカット自動検出器とEUROTECHのPG1000超精密多機能検出器を装備しています.会社の主な製品は,固体カービッドのフライスカッターと穴加工カッターです. さらに,顧客の要求に基づいて,様々な非標準的なカッター設計と生産することができます国内航空,自動車,機械,模具,プラスチック,電子機器,医療機器,その他の高精度仕上げ分野に広く使用されています."誠実さに基づく顧客優遇"というサービス哲学と"品質で生き残り,信用で発展する"という目標に基づいて,顧客に満足のいく製品やサービスを提供できる.会社には,3Cツールの様々な種類で十分な生産能力があります. 迅速な証明&配達,安定した品質!商品に興味がある...
もっと学びなさい

0

確立される年:

0

百万+
従業員

0

百万+
年間売上:
中国 Supal (Changzhou) Precision Tools Co.,Ltd 高品質
信頼証券 信用チェック RoSH サプライヤーの能力評価 企業には厳格な品質管理システムと 専門的なテストラボがあります
中国 Supal (Changzhou) Precision Tools Co.,Ltd 開発
専門的な設計チームと 先進的な機械のワークショップ 必要な製品を開発するために協力することができます.
中国 Supal (Changzhou) Precision Tools Co.,Ltd 製造業
先進的な自動機械 厳格なプロセス制御システム 電気端末を全て 製造できます
中国 Supal (Changzhou) Precision Tools Co.,Ltd 100%のサービス
卸売品と小型のパッケージは FOB,CIF,DDU,DDPです 心配事項の最善の解決策を 見つけられるようにしましょう.

品質 カービッドフライディングツール & スクエアエンドミール メーカー

あなたの条件を満たすためによくするプロダクトを見つけなさい。
事件とニュース
最新のホットスポット
Corner Radius vs Square End Mills for Interrupted Shoulder Milling
Corner Radius vs Square End Mills for Interrupted Shoulder Milling Interrupted shoulder milling is one of the operations where end mill geometry has a direct effect on edge stability. When the cutter repeatedly enters and exits the workpiece, passes across gaps, or encounters uneven stock, each tooth experiences a changing load instead of a smooth continuous cut. A square end mill can produce a sharp 90-degree shoulder, while a corner radius end mill can distribute load around the tool corner and reduce local stress. Choosing between them requires more than looking at the drawing requirement. For CNC machinists, process engineers, and purchasing engineers, the correct decision depends on the balance between required corner definition, interruption severity, tool rigidity, material, engagement, and finishing strategy. This guide compares square and corner-radius geometries for interrupted shoulder milling and explains how to diagnose edge chipping, chatter, poor finish, and unstable tool life. What Makes Interrupted Shoulder Milling Difficult? In a continuous side-milling cut, the cutting edge enters the workpiece and remains engaged in a relatively predictable way. In an interrupted shoulder operation, the edge may encounter a slot, a cross-hole, a casting irregularity, a forged surface, a previous pocket, or an open boundary. Each interruption changes the force and can create impact at entry or exit. The highest-risk conditions usually include: Repeated entry and exit at the same corner of the tool Full radial engagement at a 90-degree shoulder Thin walls or weak workholding that move during the cut Long tool overhang or poor holder runout Abrasive scale, cast skin, or hard inclusions Excessive feed or engagement at the interruption point A sharp square corner exposed to repeated impact A tool can therefore fail even when the average cutting load appears acceptable. The peak impact load, not only the average spindle load, may determine whether the edge survives. Square End Mills: Strengths and Limits A Square End Mill is the natural choice when the part requires a sharp internal shoulder or a flat-bottomed slot. Its geometry can produce a defined 90-degree corner without leaving a programmed radius at the bottom of the wall. When a Square End Mill Is Appropriate Square end mills are often considered when: The finished feature requires a sharp shoulder The toolpath uses stable, continuous engagement The workpiece and fixture are rigid The interruption is limited or can be approached with a controlled entry A separate finishing pass can protect the final corner quality The tool diameter and reach provide sufficient core strength A square tool can perform well in interrupted milling when the edge is properly supported and the engagement is controlled. It should not be rejected simply because the cut is interrupted; the severity and location of the interruption matter. Where Square Corners Become Vulnerable The tool corner is a stress concentration. During an interrupted cut, the corner may take a sudden impact as it enters the material. If the tool is also deflecting, the corner can receive more load than the other flutes. Typical results include corner chipping, a small radius appearing on the part after wear, chatter marks, or an abrupt change in surface finish. A sharp corner can also be sensitive to hard spots, scale, and thin-wall movement. If the failure is concentrated at the corner while the side cutting edges remain relatively intact, geometry and engagement should be reviewed before changing coating alone. Corner Radius End Mills: Strengths and Limits A Corner Radius End Mill includes a controlled radius between the end face and peripheral cutting edge. The radius removes the most fragile sharp corner and distributes cutting load over a larger region of the tool tip. When a Corner Radius Is Advantageous A corner-radius tool is often considered when: The cut includes repeated entry and exit The operation encounters an interrupted or uneven surface Edge chipping is concentrated at a square corner The part drawing permits a small internal radius The operation uses higher engagement or heavier roughing The process needs additional corner strength and more stable tool life The radius does not eliminate vibration or poor setup conditions, but it can reduce the severity of a localized corner impact. It may also improve the tool’s tolerance of intermittent engagement when compared with an otherwise similar sharp-corner tool. The Geometric Trade-Off The main limitation is straightforward: a corner radius leaves a radius on the finished shoulder. If the part requires a sharp 90-degree internal corner, the radius may need to be removed by a secondary operation or replaced by a square finishing tool. A corner radius can also change the effective engagement and contact area. It should be evaluated together with axial depth, radial engagement, tool diameter, and the required surface finish rather than selected based on radius size alone. How to Choose Between the Two Geometries Start With the Drawing Requirement First identify whether a sharp internal corner is functionally required or simply shown as a nominal feature. If a small radius is acceptable, a corner-radius tool may provide a more robust roughing or semi-finishing process. If a sharp corner is essential, use a square tool where practical or plan a roughing-and-finishing sequence that controls the load on the final square edge. Identify the Interruption Type Not all interruptions have the same effect. A predictable open boundary may be easier to manage than a hard casting skin or an irregular forged surface. Cross-holes and slots can create repeated impact at a known location, while uneven stock can make the load unpredictable. Record where the first damage occurs. If chipping starts at every entry point, the issue may be impact or lead-in strategy. If it appears only at a particular section of the workpiece, inspect material condition and support at that location. Match the Tool to the Operation For roughing and semi-finishing, the added corner support of a radius can be valuable when the operation is interrupted. For finishing, a square tool may be preferred if the corner specification requires it and the setup can maintain stable engagement. A practical process may use a corner-radius tool for stock removal, followed by a square end mill for the final shoulder. The two tools should not automatically use identical cutting conditions; the finishing tool may require a different engagement and a more controlled pass. Geometry, Edge Preparation, and Coating Edge Preparation A completely sharp edge may reduce cutting force in some materials, but it can be vulnerable to impact. A lightly reinforced edge may provide better stability in interrupted cuts, although excessive edge honing can increase rubbing and heat. The appropriate edge preparation depends on the workpiece, interruption severity, tool diameter, and operation. When comparing tools, request information about edge preparation rather than evaluating only flute count or coating name. Two tools with similar descriptions may behave differently if their edge preparation and carbide substrate differ. Helix and Flute Configuration Helix and flute count influence force direction, chip evacuation, and the number of teeth sharing the load. A higher flute count may support feed capacity in a light radial finishing pass, while a roughing or interrupted operation may need more chip space and a stronger core. The right balance depends on the material and engagement. A tool with insufficient flute space may recut chips, while a tool with a very thin core may lack impact resistance. Select from the broader Carbide Milling Tools range based on the actual operation rather than relying on the end mill shape alone. Coating Coating should follow the dominant failure mechanism. A coating may help manage heat, adhesion, or abrasive wear, but it cannot compensate for excessive tool deflection, a sharp corner overloaded by impact, or an unstable fixture. If the tool chips at entry, check geometry and rigidity before assuming that a coating change is the primary solution. Any coating recommendation should be validated with the specific material, tool geometry, coolant strategy, and cutting conditions. Treat supplier data as a starting reference and confirm the result on the actual machine. Parameter Strategy for Interrupted Shoulder Milling Cutting data should be treated as a starting reference for the exact diameter, flute count, coating, material grade, tool overhang, and machine setup. Do not transfer a value from a continuous side-milling operation directly to an interrupted shoulder cut without validation. Control the Peak Load at Entry Entry conditions can create the highest impact. Where the geometry allows, use a ramp, arc, or controlled lead-in instead of an abrupt radial plunge. This reduces the sudden change from no load to full engagement. If a direct entry is unavoidable, review feed and radial engagement at the entry point. A controlled reduction in engagement or a separate approach pass may protect the edge better than reducing the entire program feed. Avoid Excessive Full-Width Engagement Full-width shoulder milling creates significant radial load. In an interrupted condition, the load can change sharply as the tool crosses the gap. If possible, use a reduced radial engagement strategy for roughing and leave a controlled allowance for finishing. The correct engagement depends on the tool, material, machine, and feature geometry. Validate changes with spindle load, sound, chip form, and edge inspection rather than assuming that a smaller engagement is always better. Adjust Speed and Feed One Variable at a Time If the tool chips, do not immediately reduce both speed and feed. First determine whether the damage is impact-related, vibration-related, or caused by rubbing. A feed reduction that is too large can create a thin chip and increase rubbing, while a speed change may affect heat and resonance differently. Change one parameter at a time and document the effect. Include the location of the failure, chip appearance, surface finish, and tool condition in the record. Diagnosing Common Failure Symptoms Corner Chipping on a Square End Mill Check interruption severity, tool entry, runout, edge preparation, and whether the square corner is taking the full impact. If the drawing permits it, compare a corner-radius tool in the roughing or semi-finishing stage. If a square corner is mandatory, reduce entry shock and ensure the finishing pass has consistent stock. Chatter on a Corner-Radius Tool A radius does not remove the need for rigidity. Check tool overhang, holder condition, workholding, spindle speed, axial depth, and radial engagement. Chatter may also result from a radius that creates an engagement pattern unsuitable for the current toolpath. Uneven Wear Between Flutes Uneven wear commonly points to runout, unequal flute loading, poor holder seating, or a workpiece that is moving. Inspect the shank, collet, holder, and setup before changing the tool geometry. Poor Shoulder Finish After Roughing A roughing tool with a damaged corner or built-up edge should not be used for a critical finishing pass. Clean the feature, use a sound finishing tool, and verify that the remaining allowance is consistent. If the finish still varies, inspect vibration and workholding. Short Tool Life at a Hard Spot If damage occurs only at a particular location, investigate material condition, scale, interrupted geometry, or inadequate support. A different corner geometry may help, but the toolpath and entry strategy should also be reviewed. Common Mistakes to Avoid Choosing a Square Tool Only Because the Part Has a 90-Degree Corner A square finishing tool may be correct for the final feature but unnecessarily vulnerable during heavy interrupted roughing. Separate stock removal from final corner generation when the process requires both robustness and a sharp corner. Assuming a Corner Radius Always Solves Chipping The radius can improve corner strength, but it does not fix excessive overhang, runout, unstable workholding, poor parameters, or a damaged holder. Reducing Feed Aggressively After Chipping A large feed reduction can cause rubbing and heat. Determine whether the first damage occurred at entry, during an interruption, or under continuous cutting before making broad changes. Ignoring Toolholding The geometry selected on paper cannot compensate for poor holder cleanliness, excessive runout, or unnecessary projection. Check the actual holder and machine setup. Mixing Roughing and Finishing Requirements One tool rarely provides the best combination of high interruption tolerance, high stock-removal capacity, sharp 90-degree finishing, and final surface quality. Define which pass is responsible for each requirement. FAQ Is a corner radius end mill stronger than a square end mill? The radius removes the sharpest corner stress concentration and can improve resistance to local chipping in some interrupted operations. The actual result still depends on material, edge preparation, tool diameter, engagement, rigidity, and parameters. Should I use a corner radius for every interrupted shoulder cut? No. If a sharp 90-degree corner is required, a square end mill may still be necessary for finishing. A corner-radius tool can be considered for roughing or semi-finishing when the part permits a radius or a secondary finishing operation. Why does my square end mill chip only at the entry point? The entry may create an impact or engagement spike. Check lead-in strategy, radial engagement, feed at entry, runout, workpiece support, and the condition of the material surface at the entry location. Can changing the coating stop corner chipping? Only when the dominant failure involves heat, adhesion, or wear that the new coating is suited to control. Coating cannot correct an overloaded corner, poor rigidity, abrupt entry, or excessive engagement. What information should I provide when requesting an end mill recommendation? Provide the material grade, shoulder and interruption geometry, required corner condition, tool diameter and reach, machine and holder details, current parameters, coolant method, tool wear pattern, and photographs of the damaged edge or finished shoulder. Conclusion The choice between a corner-radius and square end mill for interrupted shoulder milling should begin with the part requirement, then consider interruption severity, edge strength, tool rigidity, engagement, and finishing strategy. A square end mill provides a sharp corner but concentrates stress at the tool tip. A corner-radius end mill distributes load more gradually and may reduce local chipping when a radius is acceptable. For demanding operations, a two-stage process can balance both objectives: use a robust geometry for interrupted roughing or semi-finishing, then use a square tool for the final shoulder when the drawing requires a sharp corner. Build parameters from the supplier’s starting range, change one variable at a time, and validate the complete process on the actual machine and workholding. If your shoulder milling process shows corner chipping, chatter, poor finish, or inconsistent tool life, Contact Supal with the material grade, interruption geometry, current tool, tool overhang, parameters, and photos of the failure. This information helps identify a practical geometry and process starting point for on-machine validation.

2026

10/06

How to Choose Carbide End Mills for Copper and Brass Machining
How to Choose Carbide End Mills for Copper and Brass Machining Copper, brass, bronze, and other copper alloys are often described as easy-to-cut materials because they are softer than hardened steel. That description can be misleading. Copper alloys can create very different machining problems depending on their purity, temper, alloying elements, work-hardening behavior, and chip form. A tool that produces a clean result in free-machining brass may rub, smear, or generate built-up edge in a more adhesive copper grade. For CNC machinists, process engineers, and purchasing engineers, reliable copper alloy milling starts with matching the tool to the actual failure mechanism. Edge sharpness, flute space, chip evacuation, workholding, coolant, and parameter validation usually matter more than simply choosing the hardest or most expensive coating. This guide explains how to select carbide end mills for copper and brass machining while reducing adhesion, burrs, heat, and unstable tool life. Why Copper and Brass Need Material-Specific Tool Selection Copper alloys combine several characteristics that influence milling stability: Copper conducts heat efficiently, so heat can move into the workpiece instead of remaining concentrated at the tool edge. However, local rubbing can still raise edge temperature and cause adhesion. Pure or highly ductile copper can produce continuous, gummy chips that are difficult to evacuate. Brass and bronze grades vary widely. Some produce short chips, while others create longer chips or abrasive particles. A dull edge may rub and smear the surface rather than shear it cleanly. Thin walls, small features, and poor workholding can amplify deflection and burr formation. The result is that “copper” or “brass” is not enough information for final tool selection. The exact alloy or grade, hardness or temper condition, feature geometry, and finishing requirement should be confirmed before adopting a production tool. Common Failure Symptoms in Copper Alloy Milling Built-Up Edge and Material Adhesion Built-up edge appears when copper or another ductile alloy adheres to the cutting edge. The tool may look sharp at the beginning of the cut but gradually develops a welded mass that changes the effective edge geometry. This can cause poor surface finish, burrs, dimensional variation, and sudden edge damage when the built-up material breaks away. Adhesion is often promoted by rubbing, insufficient chip evacuation, a dull edge, excessive dwell, or a surface treatment that is not suited to the material. Changing to a harder coating without correcting rubbing may not solve the problem. Smearing and Poor Surface Finish A smeared surface usually indicates that the tool is not shearing the material cleanly. Possible causes include insufficient chip thickness, a dull or heavily honed edge, poor tool runout, unstable workholding, or a speed/feed combination that leaves the tool rubbing instead of cutting. Burrs at Entry and Exit Copper and brass can produce burrs when the cutting edge pushes material away at the exit. Burr formation is influenced by tool sharpness, radial engagement, feed direction, workpiece support, and the condition of the edge. A finishing pass may reduce burrs, but the root cause should still be addressed in the toolpath and tool selection. Chipped Edge or Unexpected Tool Failure Carbide edge chipping in copper alloy milling is not always caused by a material that is too hard. Interrupted cuts, loose workholding, excessive runout, thin-wall deflection, collisions, and trapped chips can generate impact loads that damage the edge. If chipping is concentrated on one flute, inspect runout and setup balance before changing the carbide grade. Chip Packing and Recutting Long copper chips can remain in a pocket, slot, or narrow cavity. Once recut, they create additional heat and load, increasing the chance of built-up edge and surface scratching. Tool geometry and air or coolant direction should be selected with chip travel in mind, especially in deep features. Flute Geometry and Edge Sharpness Choose Enough Chip Space for the Operation Copper and ductile brass grades may require generous flute space so chips can leave the cutting zone before they are recut. A low-flute-count tool can be useful when chip evacuation is the primary limitation, but the correct flute count also depends on rigidity, engagement, feed, finish, and feature geometry. For a deep pocket or slot, prioritize a toolpath and geometry that provide a clear chip path. For a light finishing pass, a different flute configuration may be preferred if it provides the required surface quality without creating excess rubbing. Favor a Clean, Sharp Cutting Edge A sharp edge generally helps shear copper and brass rather than push or smear them. Excessive edge rounding can increase rubbing and heat. However, sharpness must be balanced against the risk of edge damage in interrupted cuts, cast surfaces, abrasive inclusions, or unstable fixtures. The best edge preparation is application-dependent. A stable finishing cut may benefit from a very sharp edge, while a roughing operation with impact risk may require controlled edge reinforcement. Request the intended edge preparation when comparing tools rather than judging only by the product title. Consider Polished Flutes and Rake Surfaces A smooth flute and rake surface can reduce friction and help chips slide away from the cutting edge. This is particularly relevant when the material tends to adhere or when the tool is used in a narrow cavity with limited chip clearance. Polishing alone does not replace the need for suitable flute volume, coolant, or air blast, but it can support cleaner chip transport. Coating and Substrate Considerations Copper alloy applications do not always benefit from the same coating choices used for hardened steel. The dominant issue may be adhesion and friction rather than oxidation or high-temperature wear. In some applications, uncoated polished carbide is appropriate because the sharp, low-friction surface is more important than a hard coating layer. For abrasive copper alloys, bronze grades, or materials containing hard particles, a coating or substrate selected for wear resistance may be useful. The correct choice depends on the exact alloy and failure mode. Do not assume that a coating marketed for hardened steel will automatically improve copper machining, and do not assume that an uncoated tool is correct for every bronze or filled alloy. When comparing copper tools with End Mills for Aluminum, use the aluminum tool as a reference only, not as an automatic substitute. Both material groups can be adhesion-prone, but the exact chip form, edge condition, and surface requirement may differ. Parameter Strategy for Copper and Brass Milling Start With the Actual Tool and Alloy Cutting data should be treated as a starting reference, not a guaranteed setting. The appropriate speed, feed, radial engagement, and axial depth depend on tool diameter, flute count, stickout, machine rigidity, workholding, alloy grade, and coolant or air-blast conditions. Validate the starting range on the actual machine before making it a standard process. Avoid Rubbing and Dwell If the tool spends too much time sliding along the surface, adhesion and smearing become more likely. Check whether the toolpath includes dwell at corners, excessive radial engagement, or a feed value that is too low for the selected edge geometry. A modest, controlled chip load is usually preferable to a cut dominated by rubbing, but the exact value must be validated for the tool and material. Control Chip Evacuation Direct air or coolant so chips move away from the cutting zone rather than being pushed back into the pocket. If chips are long, review flute volume, toolpath engagement, and the conditions that determine chip formation. Increasing fluid pressure without correcting nozzle direction or chip path may produce little improvement. Change One Variable at a Time When troubleshooting built-up edge, burrs, or poor finish, change only one major variable at a time: tool geometry, coating, speed, feed, engagement, or chip evacuation. Document the result. This makes it possible to identify the actual improvement instead of attributing every change to the last tool purchased. Toolholding, Workholding, and Feature Stability Even a well-selected tool can fail when the setup is unstable. Check tool runout, holder cleanliness, clamping length, and the shortest practical tool projection. Thin copper components and unsupported walls can deflect under cutting pressure, leaving burrs or dimensional error that look like a tool problem. For holes and finishing operations, coordinate the milling process with Carbide Drills and Carbide Reamers. A poor pre-hole or unstable entry can reduce the performance of the finishing tool even when the reamer itself is suitable. A Practical Selection and Troubleshooting Sequence Confirm the exact copper, brass, bronze, or copper-alloy grade and condition. Identify the dominant failure: adhesion, burrs, poor finish, chip packing, chipping, or dimensional drift. Select flute count and chip space based on engagement and chip travel, not on flute count alone. Review edge sharpness, rake surface, flute polish, coating, and substrate together. Check runout, overhang, workholding, and thin-wall support. Establish a conservative starting process and validate it on the actual setup. Adjust one variable at a time and record chip form, finish, burr condition, load behavior, and tool wear. Common Mistakes to Avoid Treating All Copper Alloys as Pure Copper Brass, bronze, and specialized copper alloys can produce very different chips and wear mechanisms. A recommendation for one grade should not be transferred automatically to another. Choosing Coating Before Identifying the Failure Mode If adhesion is the primary issue, friction and edge sharpness may deserve attention before thermal coating performance. If abrasion is dominant, the solution may require a different substrate or wear-resistant coating. Diagnose first. Using a Dull Tool for a Finishing Operation A worn edge can rub, smear, and create burrs even when the tool still appears usable. Replace or recondition the tool based on the required surface and dimensional result, not only on visible fracture. Ignoring Chip Travel in Pockets and Slots Long chips that remain in the cavity will be recut. Review toolpath direction, flute space, air blast, coolant placement, and the ability of the machine to clear chips. Copying Parameters From Steel or Aluminum Without Validation Copper alloy behavior is not identical to steel or aluminum. Use supplier data as a starting reference and confirm the process on the actual machine, workholding, and material grade. FAQ What type of carbide end mill is commonly used for copper? A sharp, low-friction tool with suitable chip space is often considered for copper, but the correct flute count, edge preparation, coating, and substrate depend on the exact alloy and operation. Confirm the choice against the material grade and feature geometry. Why does copper create built-up edge on the tool? Built-up edge is commonly associated with adhesion, rubbing, heat concentration, poor chip evacuation, or an edge condition that is not suited to the material. Review sharpness, flute polish, toolpath engagement, and validated parameters before changing coating alone. Is an uncoated carbide end mill suitable for brass and copper alloys? It can be suitable in some applications where a sharp, polished, low-friction edge is the priority. Abrasive bronze or filled copper alloys may require a different wear strategy. The exact recommendation should be confirmed for the specific grade and failure mode. How can I reduce burrs when milling copper? Check tool sharpness, runout, exit engagement, workpiece support, radial engagement, and feed direction. A finishing pass may help, but burr reduction is usually more reliable when the edge and toolpath are stable from the beginning. What information should I provide when requesting a copper alloy tool recommendation? Provide the exact alloy and condition, tool diameter and flute count, feature geometry, tool overhang, machine and holder details, current parameters, coolant or air-blast method, chip form, and photographs of the finish or worn edge. Conclusion Choosing carbide end mills for copper and brass machining requires more than selecting a standard tool for a soft material. The best starting point is to identify the alloy, failure mode, chip behavior, and setup stability. Sharp and suitable geometry, sufficient chip space, controlled friction, reliable evacuation, and validated parameters work together to reduce built-up edge, burrs, smearing, chipping, and inconsistent tool life. If your copper or brass operation has adhesion, burr, chip evacuation, surface-finish, or tool-life problems, Contact Supal with the material grade, feature geometry, current tool, parameters, and failure photos. This information helps evaluate a practical tool and process starting point for on-machine validation.
2026

10/01

超硬リーマのビビリ音とオーバーサイズ穴:トラブルシューティングガイド
カーバイドリーマーのチャタリングとオーバーサイズ穴:トラブルシューティングガイド リーミングは、多くの場合、単純な仕上げ加工として扱われます。穴を開け、リーマーを回せば、寸法と表面仕上げが改善されると期待されます。実際には、カーバイドリーミングは、アローワンス、芯出し、剛性、クーラント供給、刃先形状、およびパラメータの安定性に敏感です。これらの変数のいずれかが間違っていると、チャタリングマーク、オーバーサイズ穴、真円度の低下、テーパー穴、刃先の欠け、または予期せぬ短い工具寿命が発生する可能性があります。 CNC加工オペレーター、プロセスエンジニア、および購買エンジニアにとって、重要な点は次のとおりです。リーマーは、すべての穴あけ問題を修正するわけではありません。リーマーは準備された穴を改善できますが、深刻な芯ずれ、傷、アンダーサイズ、フレアした、または不安定な事前穴を確実に修正することはできません。このガイドでは、カーバイドリーマーのチャタリングと穴公差の問題を段階的に診断する方法を説明します。これにより、是正措置は推測ではなく、故障モードに基づいたものになります。 リーミングの問題が診断しにくい理由 カーバイドリーマーは、複数の刃先を同時に切削し、わずかな量の材料しか除去しません。この加工は、穴あけやフライス加工と比較して軽微であるため、多くの工場ではリーミングは寛容であると想定しています。実際には、わずかなストックアローワンスとタイトな公差目標により、プロセスは寛容ではなくなります。 リーミングアローワンスが小さすぎると、工具が切削する代わりに擦れる可能性があります。アローワンスが大きすぎると、刃先が過負荷になる可能性があります。穴あけされた穴がまっすぐでない場合、リーマーは既存のエラーに従うか、不均一に切削するように強制される可能性があります。ホルダーまたは固定具に剛性が欠けている場合、小さな振動が穴の内側に目に見えるチャタリングラインとして現れる可能性があります。 これが、同じリーマーが、同じ公称穴径の別のセットアップで失敗する一方で、あるセットアップで優れた仕上げを生成できる理由です。 カーバイドリーミングにおける一般的な症状 穴の内側のチャタリングマーク チャタリングマークは通常、穴壁に繰り返し現れるらせん状または多角形のようなパターンとして現れます。これらは、切削中に工具、ホルダー、ワークピース、または機械構造が振動していることを示します。チャタリングは、過剰なアローワンス、不十分な剛性、不十分な芯出し、不適切な速度、または不安定な事前穴によって引き起こされる可能性があります。 リーミング後のオーバーサイズ穴 オーバーサイズ穴は、工具の振れ、芯ずれ、過剰な切削圧力、熱膨張、またはリーマーと穴壁の間に閉じ込められた切りくずによって引き起こされる可能性があります。オーバーサイズ穴が一貫して繰り返される場合は、リーマーの直径が間違っていると仮定する前に、振れを測定し、事前穴の状態を確認してください。 粗い表面仕上げ リーミング後の粗い表面仕上げは、溶着エッジ、不十分なクーラント、切りくずの再切削、不十分なドリル準備、または摩耗した刃先から生じる可能性があります。リーマーが不均一なストックを除去するように強制されると、工具が鋭利であっても表面仕上げが悪化することがよくあります。 短いまたは一貫性のない工具寿命 同じ用途で、あるリーマーが別のリーマーよりもはるかに長持ちする場合、機械セットアップ、穴準備、クーラント供給、および部品材料のばらつきを確認してください。工具コーティングとカーバイドグレードは重要ですが、プロセスの不安定性はしばしば最初に排除すべきことです。 刃先の欠け カーバイドリーマーの刃先の欠けは、しばしば衝撃、断続切削、過剰なアローワンス、不十分な入り込み、またはワークピースの硬い介在物を示します。リーマーは仕上げ工具です。大きな穴あけエラーを修正したり、重いストックを除去したりするように設計されていません。 根本原因1:不適切なリーミングアローワンス 事前穴アローワンスは、リーミングにおける最も重要な変数の一つです。ストックが少なすぎると、擦れ、熱、および粗い仕上げを引き起こす可能性があります。ストックが多すぎると、刃先に過負荷がかかり、チャタリングや欠けを引き起こす可能性があります。 すべての直径、材料、およびリーマー設計に適合する普遍的なアローワンスはありません。開始原則として、小径穴は一般的に小さいアローワンスを必要としますが、大径穴はより多くのストック除去に耐えることができます。ただし、正しい値は、ワークピース材料、穴の深さ、工具形状、クーラント方法、および公差目標に依存します。他の加工の値からコピーするのではなく、常に実際の機械と固定具でアローワンスを検証してください。 トラブルシューティングの際は、リーミング前の実際の穴あけ穴の直径と最終目標を比較してください。事前穴のサイズが部品ごとに異なる場合、リーミングの結果も異なります。 根本原因2:不十分な事前穴品質 リーマーには安定したガイドが必要です。穴あけされた穴がすでに位置ずれしている、テーパーになっている、傷がついている、またはひどく加工硬化している場合、リーミングははるかに困難になります。 リーマーを非難する前に、穴あけプロセスを検査してください。ドリルが円形できれいな穴を生成しているか、切りくずが壁を傷つけているか、ドリルが入り口でウォークしているかを確認してください。穴あけプロセス制御のために、カーバイドドリルとリーマーは、無関係な工具としてではなく、システムとして選択されるべきです。 ドリルがひどい切りくずの傷や一貫性のない穴のサイズを残す場合、リーマーは欠陥を修理するのに十分な制御を持っていない可能性があります。まず穴あけの安定性を改善し、次にリーミングパスを評価してください。 根本原因3:振れと芯ずれ 振れは、オーバーサイズ穴と不均一な工具摩耗を生成する最も速い方法の1つです。ホルダーまたはスピンドルのわずかな振れは、他の刃先よりも1つの刃先に多くの作業をさせる可能性があります。これにより、不均一な切削圧力、真円度の低下、および工具寿命の短縮が生じます。 可能な場合は、工具シャンクと切削部近くの振れを測定してください。また、ホルダーの状態、コレットの清浄度、スピンドルの状態、および工具が十分な接触長でクランプされているかを確認してください。精密穴の場合、工具保持システムはリーマー自体と同じくらい重要です。 芯ずれは、リーマーがスピンドルパスと同軸でない穴に入るときにも発生する可能性があります。これは、以前の加工、固定具、または長リーチセットアップがたわみを導入する場合に一般的です。 根本原因4:速度、送り、および切削安定性 リーミングパラメータは、擦れや振動なしできれいに切削できるほど安定している必要があります。速度が高すぎると、熱が増加し、一部の材料でチャタリングが悪化する可能性があります。送り速度が低すぎると、切削ではなく擦れが発生する可能性があります。送り速度が高すぎると、刃先に過負荷がかかり、表面仕上げが悪化する可能性があります。 トラブルシューティングの場合、一度に1つの変数を調整してください。チャタリングが発生した場合、速度をわずかに下げることで役立つ可能性がありますが、剛性とアローワンスがすでに合理的である場合に限ります。工具が擦れて熱を発生する場合、安全な範囲内で送り速度を上げることが切削作用を改善することがあります。パラメータの変更は、実際の部品材料での試削りによって検証されるべきです。 一般的な速度と送りテーブルを最終値として使用することは避けてください。これらを開始参照として扱い、穴のサイズ、深さ、機械の剛性、クーラント、および公差要件に基づいて調整してください。 根本原因5:クーラントと切りくず制御 リーミングは穴あけよりも材料除去量が少ないですが、切りくずは依然として重要です。穴の中に閉じ込められた細かい切りくずや粒子は、壁を傷つけ、刃先を損傷する可能性があります。クーラントは、切りくずを洗い流し、熱を減らし、切削ゾーンを安定させるのに役立ちます。 ブラインド穴の場合、切りくずの排出は、切りくずが穴の底から出るスペースが限られているため、より困難になります。クーラントの方向、圧力、および流量は慎重に確認されるべきです。穴あけから切りくずが穴に残っている場合は、リーミング前に穴を清掃またはフラッシュしてください。 クーラントの濃度とろ過も重要です。汚染されたクーラントは、研磨粒子を穴に戻し、表面仕上げと工具寿命に影響を与える可能性があります。 根本原因6:リーマー形状と用途適合性 異なるカーバイドリーマーは、異なる用途のために設計されています。フルート設計、リード角、マージン設計、刃先準備、およびコーティングなどの要因は、切削安定性と切りくず排出に影響を与える可能性があります。 スルーホール用のリーマーは、ブラインドホールで同じように動作しない場合があります。アルミニウム用に最適化されたリーマーは、ステンレス鋼や硬化材料には理想的ではない場合があります。長いリーマーは、剛性と振れに特別な注意が必要になる場合があります。 サプライヤーとリーマーの問題について話し合うときは、ワークピース材料、事前穴の直径、目標公差、穴の深さ、スルーホールまたはブラインドホールの状態、クーラント方法、現在のパラメータ、および可能であれば穴表面の写真を提供してください。この情報は、解決策が形状変更、パラメータ変更、またはプロセス修正であるかどうかを判断するのに役立ちます。 実用的なトラブルシューティングワークフロー ステップ1:事前穴を測定する 仕上げ穴を確認する前に、リーミング前の穴あけまたはボーリングされた穴を測定してください。可能であれば、直径、真円度、直角度、および表面状態を記録してください。事前穴が不安定な場合は、まずそれを修正してください。 ステップ2:工具の振れを確認する 実際のホルダーでの振れを測定してください。シャンク、コレット、およびホルダーを清掃してください。損傷したホルダーまたは摩耗したコレットを交換してください。振れが減少し、オーバーサイズ穴が改善された場合、リーマーは主な原因ではありませんでした。 ステップ3:アローワンスを確認する 実際の事前穴の直径とリーマーのサイズを比較してください。部品間でアローワンスが異なる場合は、穴あけまたはボーリング加工が一貫性がない理由を特定してください。 ステップ4:切りくずと表面仕上げを検査する 穴に閉じ込められた切りくず、傷、または擦れマークを探してください。切りくずの傷が現れた場合は、クーラントフラッシングと事前穴の清掃を改善してください。 ステップ5:パラメータを段階的に調整する 速度、送り、またはクーラントを一度に1つの要因ずつ変更してください。結果を記録してください。現在のセットアップが明らかに不適切でない限り、工具形状とパラメータを同時に変更することは避けてください。 ステップ6:工具選択を確認する プロセスが安定しているが問題が残る場合は、リーマーの形状、コーティング、フルートスタイル、および刃先準備を確認してください。関連する機械加工および仕上げ用途のために、Supalはより広範なCNCプロセス計画のためにカーバイドフライス工具も提供しています。 避けるべき一般的な間違い 間違い1:リーマーに悪い穴を修正することを期待する リーマーは仕上げ工具であり、レスキューツールではありません。穴あけされた穴がひどく偏心している、テーパーになっている、または傷がついている場合は、まず事前穴を改善してください。 間違い2:振れを無視する 振れは、正確なリーマーをオーバーサイズに切削させる可能性があります。工具自体が不正確であると仮定するのではなく、常に実際のホルダーで工具を測定してください。 間違い3:アローワンスが小さすぎる 材料が少なすぎると、擦れ、熱、および粗い仕上げが発生する可能性があります。工具は、不規則なストックを研磨するのではなく、切削する必要があります。 間違い4:アローワンスが大きすぎる 材料が多すぎると、刃先に過負荷がかかり、チャタリング、欠け、または真円度の低下を引き起こす可能性があります。 間違い5:プロセスを確認する前にリーマーの直径を変更する 穴が振れ、芯ずれ、またはチャタリングのためにオーバーサイズになっている場合、工具直径を変更しても根本的な問題は解決しない可能性があります。 FAQ 私のカーバイドリーマーがオーバーサイズ穴を生成するのはなぜですか? 一般的な原因としては、振れ、芯ずれ、過剰なアローワンス、不安定な事前穴品質、閉じ込められた切りくず、または熱的影響が挙げられます。リーマーの直径が不正確であると仮定する前に、振れと事前穴のサイズを測定してください。 リーマーはドリルのウォークを修正できますか? 限定的な程度までです。穴あけされた穴が大幅に位置ずれしているか、まっすぐでない場合、リーマーは既存のエラーに従う可能性があります。まず穴あけまたはボーリングプロセスを改善してください。 リーミング中にチャタリングが発生するのはなぜですか? チャタリングは、過剰なアローワンス、不十分な剛性、不適切な速度、長い工具オーバーハング、不安定な事前穴形状、またはスピンドルと穴の間の不十分な芯出しから生じる可能性があります。 リーマーのチャタリングを止めるために速度または送り速度を減らすべきですか? 速度を下げることが役立つ場合もありますが、常に最初の解決策ではありません。まず振れ、アローワンス、ホルダーの剛性、および事前穴の品質を確認してください。送り速度が低すぎると、擦れの原因にもなります。 リーマーのトラブルシューティングサポートを依頼するとき、どのような情報を提供すべきですか? ワークピース材料、事前穴の直径、目標直径と公差、穴の深さ、スルーホールまたはブラインドホールの状態、クーラント方法、現在の速度/送り、工具オーバーハング、ホルダータイプ、および穴表面または摩耗したリーマーの写真を提供してください。 結論 カーバイドリーマーのチャタリング、オーバーサイズ穴、および短い工具寿命は、通常、工具の問題だけでなく、プロセスの問題です。最も効果的なトラブルシューティングシーケンスは、事前穴を測定し、振れを確認し、アローワンスを確認し、表面マークを検査し、パラメータを一度に1つの変数ずつ調整することです。 不安定な穴公差、チャタリングマーク、または短いリーマー寿命に直面している場合は、Supalに連絡して、ワークピース材料、事前穴の状態、目標公差、現在のパラメータ、および故障写真を提示してください。Supalは、根本原因がアローワンス、振れ、クーラント、リーマー形状、または全体的なプロセス安定性であるかどうかを評価するのに役立ちます。

2026

09/29